 American
Iron and Steel
Institute
Past GDIS™ Presentations
Past GDIS Presentations
The ladder frame used in PU/SUV is a key component for aspects of vehicle performance such as rough road durability and robustness. At the same time, meeting CAFE regulation and achieving carbon neutrality calls for further weight reduction. Our next generation frame installed in new PU/SUV models adopts an integrated differential thickness structure using new curved (non-linear) tailor welded blanks technology featuring high productivity and reliability. Small radius curved welding enables more efficient reinforcement using steels with larger variation in thickness and material composition, resulting in a weight reduction of approximately 14kg compared to the current structure that welds the reinforcement plate on the main body.
The Auto/Steel Partnership (A/SP) stamping team has been working to better understand advanced high-strength steel (AHSS) and 3rd Gen AHSS material behavior and improve AHSS forming models to predict the forming tonnages more accurately for these steels. The mass reductions, particularly in the automotive Body-In-White (BIW) structure, continue to dominate the list of vehicle electrification enablers. The combination of high-strength and high-ductility of the 3rd Gen AHSS are ideal for vehicle component and assembly lightweighting. Understanding the forming nuances of stamping these steels will facilitate the design and manufacture of lightweight components that enable automakers to achieve electric vehicle range, emissions, and performance targets.
The A/SP stamping team has been working to better understand AHSS and 3rd Gen AHSS material behavior and improve AHSS forming models to predict the forming tonnages more accurately for these steels. The team recently completed the second phase of this work, which focused on assessing applied press tonnage through the complete press stroke of a pseudo-automotive component. The components were stamped using a Nidec/Minster servo press and a Martinrea die, which is an extended hat section with an in-die spring-back control feature called an “S-Corner.” In prior work, it was shown that forming simulations accurately predicted press tonnage up to the point of die closure, but the simulations did not include the work done after die closure to obtain desired dimensional quality. This work will demonstrate that: a) the S-corner is an effective spring-back countermeasure, b) will highlight the effects of adding energy to the part without increasing the press force by delaying the time the press/die system is in dwell, c) show an ideal press geometry, as well as the stamping cross section and d) justify further work to improve press tonnage prediction.
This presentation will summarize work of the Auto/Steel Partnership (A/SP) project, Die Wear Testing – Phase II using 1180 GI & EG coated sheet steel. This project is focused on obtaining new knowledge by comparing/calibration test results with die wear simulated sliding energy calculations, as well as relationship of wear vs. sliding energy density of 3rd Gen advanced high-strength steel (AHSS) stampings. The team utilizes a die wear sliding tabletop tester to do a series of experimental test on 3rd Gen ultra high-strength steel (UHSS) of galvanized iron (GI) and electro galvanized (EG) coated steel sheets to continue improvement of forming die material, surface treatment, lubricant and coating. Cast Caldie with/without ionitride and physical vapor deposition (PVD) Ionbond 90 coating. The team will examine through optical microscopy, scanning electron microscope (SEM), weight measurements any wear and/or surface build up upon the die wear pin and any damage on either the sheet and/or the pin. The collection of friction data and integrated sliding energy for each testing case will be process.
On cold formed applications Mubea is currently using micro-alloyed advanced high-strength steel (AHSS) to produce blanks and formed parts with variable gauges. With the general idea to close the gap in the TRB material portfolio between the maximum strength cold form material (CR500 TRB) and press hardened steel (PHS) applications, Mubea TRB developed the material families MTS (Mubea Tailor Softened) and MTH (Mubea Tailor Hardened).
Both new developments offer tailored mechanical properties in cold formed structural parts to satisfy the local performance requirements of the vehicle with reduced process cost.
The main characteristic of MTS material is to have two strength levels beside different gauges in one part. By choosing gauges with low rolling reductions the slightly elevated raw material mech. properties can be used to have higher strength areas with high thickness in the part. At the same time the thinner gauges will have a lower strength compared to the higher gauge area. This can be used to design intrusion beams with cold form material without the high cost of the hot forming process.
In case of the MTH material the higher strength is being achieved by increasing the mechanical properties to the higher strength level (yield and tensile strength) using cold rolling and the mechanism of “dislocation hardening” in defined borders. Different to the already establish TRB process for cold formed material, we are starting with a much lower (less expensive) material grade compared to the reference and we are omitting the annealing process. Both aspects are the main driver to achieve a cost reduction compared to the baseline material and contribute to CO2 reduction in the production process as well as in the vehicle use phase. Material cards for MTS and MTH material were developed for forming simulation as well as for crash simulation including failure.
Jill Fuel discussed the 2022 Honda Civic (North American Car of the Year).
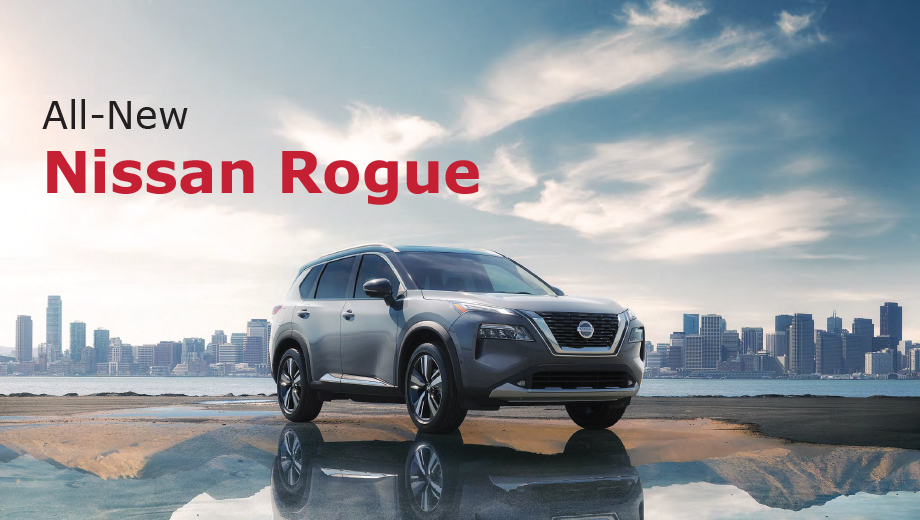
Jason Lyman and Weston Lawson discussed the 2021 Nissan Rogue.
Steel E-Motive: Development of advanced high-strength steel (AHHS) body structure for a new, fully autonomous Mobility as a Service (MaaS) vehicle.
Autonomous vehicle technologies opens up the possibilities for a significant growth in MaaS and ride sharing transportation. This paper details the development of a new body structure design for a Level 5 fully autonomous vehicle, using the latest Advanced High-Strength Steel grades and fabrication processes. The vehicle concept was created within the Steel E-Motive project, a collaboration between WorldAutoSteel and Ricardo. The vehicle has been designed with the new mode of transport in mind, with a strong focus on the user, the fleet operator and the vehicle’s operating environment. A change from human to fully autonomous vehicles removes the requirement for driver interfaces and controls and enables occupants to be seated in unconventional locations and orientations. Legislative requirements such as driver vision and obscuration are also removed, which opens up further freedoms such as the ability to place structure in existing glazed areas. These freedoms have enabled the creation of a unique and spacious transportation environment, whilst being compact in size and agile around city center. The vehicle is designed to be compliant with global high-speed crash and safety requirements and with occupants positioned in unique positions and orientations, a revised approach to the crash load management and occupant protection is required. This paper details the design of the Steel E-motive vehicle and body structure, the steel grades and technologies used and the performance achieved.
Kate Namola discussed Toyota Motor NA’s weldability investigation of 3rd Gen AHSS for automotive manufacturing. Presentation not available.
Most automotive companies have public-facing goals to improve the sustainability performance of their companies and products due to drivers from government, investors, non-profits organizations, and customers. For example, Ford has a goal of becoming “carbon neutral globally by 2050” [1]. GM’s vision is “zero crashes, zero emissions and zero congestion” and has a published goal to “Strive for at least 50% sustainable material content in our vehicles by 2030” [2]. Companies increasingly recognize that meeting their goals will entail assessing and reducing the impacts of their supply chains, including the production of automotive materials, like steel, aluminum, and plastics. However, given that the sustainability movement and associated frameworks are rapidly evolving, they may not know where to start or focus. Furthermore, there can be confusion around emerging sustainability topics, like decarbonization, Scope 1, 2, and 3 greenhouse gas emissions, Science-based Targets, net zero, carbon neutrality, and life cycle assessment. This presentation strives to provide clarity about key sustainability concepts, trends relevant to the automotive market, and the role of material suppliers. As steel is the largest share by weight in today’s vehicles, the steel industry has a key role to play in an automotive company’s strategy. The American steel industry has been striving to reduce impacts for decades and is actively working on strategies to not only reduce its own impacts, but also to further improve the environmental performance of steel products. This presentation will also provide details on the American steel industry’s sustainability performance and the path ahead on sustainability.
[1] https://corporate.ford.com/microsites/fordtrends/sustaining-sustainability.html
[2] https://www.gmsustainability.com/esg-management/goals-and-progress.html
For 30 years, TWB has been expanding technology and capability to meet the growing demands for lightweighting and improved crashworthiness. Starting in 1992, the first tailored blanks produced were common grades, only changing the thicknesses across the blanks, these components were doors and bodysides, driven by requirements on material savings and part consolidation.
Over time, with customers and regulations demanding safer and more fuel-efficient vehicles, many advancements in material grades, joining and manufacturing processes have occurred. The presentation will focus on the newest developments in tailor welded blanks and how they advance the adoption of advanced high-strength steel (AHSS).
Today, welded blanks in light duty frames have allowed for the cost-effective utilization of AHSS to meet crash energy management and performance goals, while offering a lighter weight alternative. New unique welded blank applications have been applied in battery electric vehicles to enable efficient steel designs. AHSS grades account for many of the welded blanks produced today, commonly joined to other AHSS grades or HSLA grades. Recent work has been completed to demonstrate future welded blank applications can include 3rd Gen steels. And finally, the HotWire+ process is now in production, which eliminates the ablation requirement when welding AlSi coated PHS.
The past 30 years of TWB have been full of milestone developments providing increased value to the OEM and the customer, the next years are projected to be as full of innovation as the last, with TWB positioned to provide tailor welded solutions for the vehicles of the future.
OEMs are challenged with securing the battery cells/modules (energy storage) within the BEV in a safe and cost-efficient manner. The energy storage components must be protected from a multitude of crash and impact scenarios as well as extreme environmental exposure and do so in a cost and package efficient manner. KATCON, a Leading Global Tier 1 Supplier of Automotive Exhaust System Components, recognized the opportunities and threats that the emerging BEV market presents. Together with their partner, Forward Engineering, the team set out to develop a new family of Cost Effective, Flexible, Scalable HV Battery Enclosure Solutions.
In this presentation, the team will share the results of this fast-track development process. Starting with a clean sheet of paper and the latest and most stringent OEM Technical and Global Regulatory Requirements, the team has developed a Multi Material HV Battery Enclosure (MMBE) design which is lighter and more cost effective than incumbent aluminum designs. Key to the outstanding crash performance and cost effectiveness of this new MMBE design was the smart application of a variety of high-performance Advanced and Ultra High Strength Steel Alloys and cost-efficient forming technologies. The team from ArcelorMittal played an important role in alloy selection as well as joining and forming technologies. This innovative design outperforms the incumbent design at a projected 26% mass savings and 14-16% cost savings.

The development of the 3rd Generation of advanced high-strength steels (AHSS) has opened new avenues for the product design of automotive lightweight components but the methodologies to fully exploit their superior mechanical properties have been lagging behind. The traditional in-plane forming limit curve (FLC) remains the standard engineering tool for formability assessment and leads to an overly conservative product design. The present study provides insight into the effect of tool contact pressure in three-point bend simulations that served for the development of a novel instability framework to capture the delay in material localization. It is demonstrated that both the magnitude and the boundary condition of how the contact pressure is applied governs the formability gain. An analytical-numerical stretch-bend model was developed which successfully captures the increase in the forming limit strains studied in Marciniak, Nakazima, stretch-bend and V-bend tests of a 3rd Gen AHSS with a nominal tensile strength of 1180 MPa. Application to a structural B-Pillar technology demonstrator correlates well with the forming trials and identifies false positives which were erroneously flagged for splitting when relying on the conventional FLC.
Note: This talk is part of to the AISI Automotive Program Project

Advanced high-strength steel (AHSS) is often illustrated in the Steel Strength-Ductility Diagram. Both academia and industry frequently refer to such a diagram to not only concisely categorize the evolving AHSS generations but also to direct the future development objectives. Nevertheless, with various new AHSS developed in recent years, the diagram is considered too simplified to represent the sophisticated tensile properties of these AHSS in the practical applications: that is, the experimental data are typically characterized at a quasi-static uniaxial strain rate at room temperature. The present work focuses on investigating how the temperature and strain rate affect the tensile properties of AHSS and correspondingly shift their distributions in the diagram. The target AHSS includes two dual phase (DP) steels, two quenched and partitioned (Q&P) steels and two austenitic steels. The results illustrate in the diagram how diverse the temperature and strain-rate dependencies of different AHSS can be. Concisely, with the temperature rising by either the external or the adiabatic heating, the Q&P and DP steels exhibit their tensile properties varying from a valley to a peak, while the two austenitic steels behave monotonic property trajectories towards two different directions. Furthermore, behind every turning of the property trajectories, there are multiple instantaneous effects, either favoring or opposing, acting together to determine how the materials behave at that moment. Particularly, the Q&P steels can be affected by the evolving thermal softening, dynamic strain aging, and transformation-induced plasticity (TRIP) effects during different temperature and strain rate ranges. Further understanding of the inter-relationship between strain rate, temperature, and material behavior, including the TRIP-effect reactivation, offer future paths to further optimization of AHSS designs for automotive applications.

In sheet metal forming simulations, a material card refers to a data-file that has, at minimum, information about hardening curve, yield locus, and fracture criteria. Depending on the requirements, a material card may have information about strain rate sensitivity, unloading modulus variation, the transient Bauschinger effect and permanent softening (as described by Yoshida and Uemori), and edge crack sensitivity. In addition to the “material card”, more information about the process can be included in the simulation: friction between the sheet and the tool as a function of sliding velocity, pressure, temperature; press kinematics, elastic deflection of the tooling and the press.
Each additional data-set will require time and expense. In this paper, the authors introduce “multi-level” material cards for different phases of sheet metal forming process developments. The idea is proven with stamping experiments using a 3rd Generation Advanced High-Strength Steel (AHSS).

The goal of this study is to understand the performance of additively manufactured (AM) die inserts in stamping applications. Stamping of 50,000 symmetrical U-bend parts made from 1 mm thick Dual Phase 980 sheet steel was performed in a progressive die with one side of the tool fabricated from Maraging Steel AM material and the other side fabricated from conventional D2 tool steel. The additive manufactured material was fabricated using laser powder bed fusion with Maraging Steel powder. All tested inserts were coated with IB90 PVD coating.
Both inserts produced quality stampings, with no significant visual artifacts. Likewise, no significant scratches were found on either insert. On the D2 side more hairlike flow lines were visible, but no deeper scratches. The D2 insert has more wear in the area close to the die entry radius, which resulted in shallow scratches on the samples’ surface.
The AM insert has deeper and wider scratches in the general contact zone (horizontal surface of the insert), but produced samples having better surface quality since this insert has less wear in the area close to the die entry radius. These results indicate that AM produced inserts have strong potential to be employed in die components for stamping of High Strength Steels.

Liquid metal embrittlement (LME) cracking during resistance spot welding (RSW) is a challenge restricting the application of zinc coated 3rd Gen AHSS in automotive structural components. From a production perspective, the potential for LME cracking in a spot weld has two related aspects, first is the steel’s susceptibility to LME cracking and the second is whether LME will manifest during RSW. The Auto/Steel Partnership (A/SP) has developed a test methodology to assess the LME susceptibility of steels using a production-like RSW process, which addresses both aspects. The Rapid LME test is low-cost rapid test that is useful in quickly determining the risk of LME cracking in homogeneous and heterogenous multi-steel stackups. To validate the effectiveness and repeatability of the Rapid LME Test, A/SP applied the test to 12 carefully chosen steel stack-ups comprised of homogenous and heterogeneous 3rd Gen AHSS and mild steel. The results showed that the cracking severity rating from the Rapid LME Test in homogeneous joints is a good indicator for the cracking severity in heterogeneous joints. However, it was found that in the heterogenous stack-ups, the fixed weld schedule used in the Rapid LME Test was not able to produce weld nuggets that met the general acceptance criteria for meaningful cracking severity comparison, due to the large materials resistivity and thickness differences. A new supplementary method to Rapid LME Test, called Weld Lobe LME Test, was developed to evaluate the cracking severity in heterogenous joints. The more production-representative weld schedules adopted by Weld Lobe LME Test was found to effectively differentiate the cracking severity in heterogenous joints. To thoroughly assess a material’s LME cracking susceptibility in both homogeneous and heterogenous joining conditions, a combination of Rapid LME and Weld Lobe LME tests is recommended. As their characterization methods of cracking severity are essentially identical, future work of this project will focus on establishing recommended crack acceptance criteria.

Resistance spot welds experience complex loading conditions in vehicle crash events. Performing mechanical tests considering a range of loading modes on spot-welded connections can help to better understand the relationship between failure characteristics and common spot weld performance indices such as strength and energy absorption capability. In this study, the mechanical performance and failure behavior of resistance spot welds from two grades of third generation advanced high strength steels (3G-AHSS), designated 3G-980 and 3G-1180, were evaluated by performing KS-II mechanical tests which impose combined/mixed loading on the joints. A novel triangulation technique coupled with digital image correlation was developed for more accurate tracking of local nugget locations during the tests which improved the accuracy of the energy absorption calculations. It was shown that propagation of the cracks into the fusion zone of the 3G-1180 spot welds restricts their capability to absorb energy via deformation of the nugget in the tensile direction, especially within tensile-dominated loading orientations. Correlation of spot weld failure modes and absorbed energy values revealed that full nugget pullout failures exhibited superior energy dissipation value during failure and are favored over partial pullout failures with low plug ratios.
If you have feedback about the GDIS™ past presentation tool, please email Sarah Burns at sburns@steel.org.