 American
Iron and Steel
Institute
Past GDIS™ Presentations
Past GDIS Presentations

Non-Equilibrium Thermodynamic Modeling to Aid Materials Design for Quench and Partition (Q&P) Steels
In support of a scientific foundation for the predictive design of composition and processing of quench and partition (Q&P) martensite/austenite TRIP steels, theory of coupled diffusional/displacive transformation is experimentally calibrated to control austenite carbon content and its associated mechanical stability. The calibrations are based on highly accurate experimental measurements using electron microscopy, high- energy x-ray diffraction and 3D atom probe tomography to quantify the amount and carbon content of retained austenite as a function of Q&P treatment. Varying the initial quench temperature to vary the initial retained austenite amount, it is demonstrated that carbon partitioning is affected by the direction of motion of the interface, favoring greater C partitioning for BCC->FCC motion. The variation in partition temperature is shown to have the maximum effect the austenite carbon content and its stability. The influence of processing parameters and alloy composition on the final Q&P microstructural characteristics are predicted via the developed mechanistic models and validated with a new series of experimental alloys. The effect of change in the microstructural features (phase composition, phase stability) on the mechanical properties would be discussed.
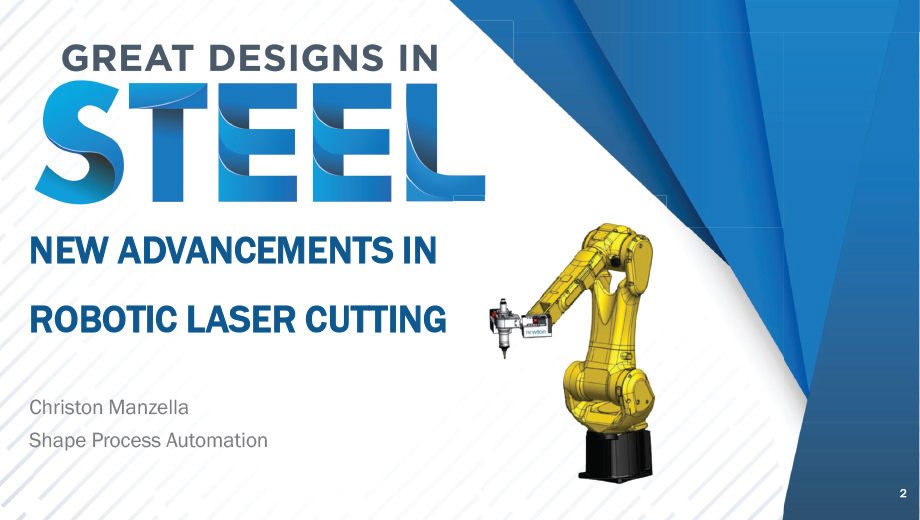
Since our first application of inline robotic laser cutting on the 2019 RAM 1500 hot stamped door ring, the industry is now focused on next generation advancements in overall equipment effectiveness. New process innovations combined with robust automation solutions allow for next generation door ring laser cutting machines to have increased performance, throughput, part to part quality and process robustness. We will explore the current obstacles of laser cutting in relation to upstream and downstream processes such as the blank trimming, furnace variables, hot forming press, die changes, and touch base on theoretical solutions to overcome these process variables. There are many laser cutting avenues that compliment other value added trim processes such as near net shape, in-die trim and predeveloped holes. Finding the right balance will ensure industry best practices are used in future light weight cost effective hot stamp door ring solutions.
Steel content for automotive applications represent the fundamental building blocks that OEMs and their tier 1’s suppliers continue to rely on to meet the evolving needs of the North American auto landscape. Advanced grades of steel show no signs of slowing down with innovation in its production, forming, and applications within the vehicle. The Ducker Study builds on several past iterations to determine current content (demand Pounds per Vehicle) by grade of steel for all NA produced light vehicles as well as scenario based forecasts for materials thru 2025.
There is a growing need to efficiently and accurately characterize next generation advanced high-strength steels (AHSS) for virtual prototyping and to predict the response of automotive structural components in crash events. The focus of the present study is to consider two next generation steels of 980 and 1180 MPa strength to develop the experimental test methodology to characterize and predict the material behavior for forming and crash applications. Advances have been made in the determination of the hardening response to large strains and to predict the formability and fracture curves in stress states ranging from shear to biaxial tension with an emphasis on plane strain bending. This project is a collaboration with SMDI and Honda Research Americas and will detail the fracture characterization and methodology used in the virtual design and tooling try-outs for a full-scale 3rd Gen B-pillar for a mid-size SUV.
Three failures can be found on drawn parts in the stamping productions. One is the necking and split on the walls of the drawn part that can be predicted with the Forming Limit Diagram (FLD), another one is the necking at the tangent point of a drawn part radius that is controlled by the material n value. These two failures are all caused by the material plastic instability. The third one is the fractures of advanced high-strength steel (AHSS) on part radii when the materials are subjected to an excessive bending under tension load. The failure criterion has yet to be developed to control the issues in stamping productions. In the current study, the fracture limits of four grades of AHSS, i.e. DP590, DP780, DP980 and DP1180, were studied with a simulative 90 degree stretch bending tests and various tool radii (from 1.0mm to 14.0mm). The DIC equipment was used to measure the surface strains and determine the fracture limits. On the basis of test results, the failure criterion has been developed for the four AHSS grades in terms of the permissible tensile strains of materials when they are on different tooling radii (R/t).
AISI’s Hesham Ezzat discussed the role of steel in future mobility.
NEXMET® 1000 is a commercialized 3rd Generation AHSS innovatively developed by AK Steel. With significantly improved elongation at higher ultimate tensile strength, NEXMET® 1000 offers OEM customers a promising solution for the lightweighting goals. To demonstrate stamping formability with NEXMET® 1000, a systematic experimental analysis was conducted to generate the forming limit curves at various thicknesses. The formability was then verified with finite element simulations and through actual component stamping. Edge stretchability and its sensitivity to hole punching configurations (punch profile, cutting clearance, etc.) was evaluated with both in-plane and out-of-plane hole expansion tests. In order to understand deformation induced plasticity phenomena in NEXMET® 1000, neutron diffraction and 3D digital image correlation (DIC) techniques were utilized to measure the evolution of constituent phase transformation at different stain paths.

The continuing expansion in the application and use of advanced high-strength steels (AHSS) in automotive vehicle structures requires increased attention relative to engineering, design and manufacturing to effectively take advantage of the superior performance characteristics of these steels. Additionally, the needs for both local and global formability must be properly balanced for efficient component manufacturing along with the added consideration of in-vehicle structural performance. It has become increasingly evident that the focus on a select group of mechanical properties and manufacturing performance metrics, e.g., yield strength, tensile strength, elongation, n-value, FLD, etc., has proven inadequate for an increasing number of applications. This talk will examine the continued development direction of selected advanced steel classes, namely press hardened steel and multi-phase steels, with a focus on property optimization via microalloying techniques and associated process strategies. Novel grade classifications with improved properties for applications are proposed for adoption within the global automotive industry.
April Bagley discussed Stellantis’ (formerly FCA) 2019 Jeep Wrangler.
AISI’s Brandie Sebastian discussed the life cycle assessment (LCA) GHG consequences of lightweighting with aluminum over advanced high-strength steel (AHSS).
The 3rd Gen advanced high-strength steels (AHSS) combine excellent strength and formability that can lead to a weight savings of between 10 and 20% in a vehicle, compared to existing Dual Phase (DP) grades. Because of their superior properties, 3rd Gen AHSS grades can absorb more energy during crash events and deform in a controlled manner while using lesser steel. At the same time, it can be used to stamp parts that otherwise would be difficult to form with conventional high strength steels. These properties make 3rd Gen AHSS ideal for use on many structural parts of the Body-in-White (BIW) such as front rail and B-pillars. However, weldability of 3rd Gen AHSS has been an important matter of discussion within the automotive industry. While, robust joining capability is crucial for any crash application with these grades, it is also important to note that these materials are compatible with the existing welding technology used for current grades in the industry.
ArcelorMittal has studied different product design parameter to deliver HF980 GI with superior weldability and minimum susceptibility to surface cracking during conventional welding. Four different welding types of resistance spot-welding (RSW), laser welding, MIG brazing and gas metal arc welding (GMAW) have been examined with no signs of surface cracks in critical zone.
Spot weld joint behavior of HF980 GI using hat shaped parts subjected to axial crush impact loading is presented in the paper. Data for different test scenarios including the effect of section geometry, part thickness, weld schedule, paint baking and weld pitch on overall joint strength and part behavior under crash loading is presented. The presentation also demonstrates the importance of different variables to be aware of when designing structural parts on a BIW with 3rd Gen steels.
The AHSS Chassis Corrosion team has completed corrosion testing on welded coupons and test specimens to evaluate various corrosion protection coatings over a 15 year simulated environment. A test procedure was developed to evaluate the corrosion in welds, crevices and exposure to gravelometer and poultice using methods consistent with procedures at FCA, Ford and General Motors.
In an effort to improve corrosion protection on chassis components which are using more thinner, higher strength steel grades, this project was designed to compare different coating for their effectiveness. The project also included the testing of weathering steels to determine whether chemistry changes in the steel substrate can be effective in reducing corrosion over a vehicle’s lifetime.
The results of this testing showed that certain coatings performed well in reducing corrosion over baseline e-coated specimens, and also showed that sample preparation can have a significant effect on improving corrosion resistance.
This presentation will show the results of the welded coupon testing, which is similar to the results attained on the “biscuit tin” test specimens tested over a 15-year simulated environment. It will also recommend potential future testing that could provide additional corrosion protection opportunities in chassis applications as well as for body structures.
There was a time that steel wheels were the only option on the market for the whole catalog of
passenger cars but it has been changing since the last few years. The aluminum wheel application became
a standard on high-end and more sophisticated middle size cars due to its flexibility on new designs and
lightweight capabilities that the steel could not cover in the past. However, nowadays, customers for
entry-level vehicles are becoming more selective and demanding the same characteristics of aluminum
on their steel wheels, prompting manufacturers to look for new alternatives in this role.
Steel material has improved over the last decade and with the improvement of simulation
software and optimization tools, the development of more complex and stylized profiles became a
possible process. Materials as AHSS, HSLA, Dual-Phase, and Ferrite-Bainite can provide an equivalent
weight of the components or even lighter, with the better performance for its application that steel can
bring and with around 60% of cost saving if compared to aluminum.
This study aims to show how Maxion brought to the market the VersaStyle, a stylized steel wheel
concept, which combined with full covers, cladding technologies and premium painting, adds a similar
style over the aluminum wheel design and a similar performance to vehicles with a more competitive
price. In addition, make a full comparison between Steel and Aluminum wheels.
Traditionally using Keeler’s equation or so-called North America Deep Draw Research Group (NADDRG) equation can’t give a good prediction of 3rd Gen at room temperature and boron steel at hot stamping temperatures. In this study, based on previously proposed ductile failure criterion (DFC), a method is proposed to model forming limit of advanced high-strength steel (AHSS). In the method, the failure is reported at localized necking while the effect of strain rate and temperature is reflected by an improved Zener-Hollomon parameter. Under isotropic yielding and plane stress assumption, the major limit strains are modeled as functions of strain paths, initial sheet thickness 𝑡0 and an improved Zener-Hollomon parameter. At the room temperature, the model becomes a function of initial sheet thickness 𝑡0 only. Same procedure of calibration and calculation of FLC can be applied on the cases of room temperature and hot stamping temperatures. The usage of the method is demonstrated on modeling FLCs of 3rd Gen steel at room temperature and boron steel at hot stamping temperatures. Comparison shows that the model can provide well representation of experimental results. Due to the easiness of calibration and consistency of the method, the method may provide a practical and consistent approach to model FLCs of AHSS.
The hot stamping process is a well-known manufacturing technology for safety and lightweight parts in automotive applications. Several process routes and windows are defined in the past years including the virtual modeling. Nevertheless, deviations from ideal process conditions can be observed very often in serial production. This can be a result of an inconstant heating process, hydraulic defects in the cooling system or uneven tool wear, just to name a few possibilities. To improve the production safety this paper shows the development of a real time process monitoring system which is fully connected to the production system. The system is gathering data from the furnace, press, automation components, the thermographic cameras and other sensors to calculate thermal- and work balances during the production in real time. After a plausibility check of the data a feasible range of values can be defined. The preprocessed data is stored in a long term database for quality assurance and is a basis further analysis. The gained information and values can be used for a better definition of the boundary conditions and their deviations for virtual modeling as well as for predictive modeling to see upcoming malfunctions or failure in advance. With this valuable information countermeasures during production can be scheduled before sudden machine downtime. This paper also shows how this process information can be linked with hot stamped part identities to achieve tracking and tracing which will be a new standard for the hot forming technology.
Welding is an essential part of any automotive assembly but determining the proper placement of welds can be a time consuming and difficult process. At the same time, there is a strong need to decrease the overall number of welds in automotive assemblies to reduce manufacturing cost and time without sacrificing structural integrity. The current spotweld optimization procedures used today involve much trial and error and are typically limited in capabilities. Optim welds, a multidisciplinary FEA spotweld optimization tool developed by BETA CAE Systems, the U.S. allows engineers to efficiently optimize the locations of spotwelds, including non-uniform weld distribution, on an assembly while also saving time and resources compared to current optimization approaches. Starting with a running FEA model, optim welds guides the user through the entire optimization procedure. Tools are provided to easily create and parameterize spotweld lines, while an optimization workflow is automatically generated according to user inputs. The resulting optimization is capable of handling multiple loadcases, disciplines, and solvers simultaneously, with the user being able to freely choose their preferred finite element weld representations. Non-uniform weld distribution is achieved through flagging critical welds in the model according to a user-specified threshold criterion, which are then carried over to subsequent designs automatically. Weld lines are parameterized in groups, leading to a reduction in the number of design variables and total optimization time. At the same time, the use of critical welds strategically places welds in important locations. Model symmetry can be defined to ensure weld placement is feasible for production. A case study with a simplified vehicle model using frontal and side crash loadcases was performed. Results after 77 designs showed a reduction of 270 welds (4%) while still meeting performance targets.
Significant advances in processing of hot stamped Laser Welded Blanks (LWB) have enabled the industry to recently apply some of the most challenging multi-seam door ring designs. The all-new 2019 RAM 1500 utilizes the world’s most complex six-seam design. These advancements have been possible through breakthrough solutions in both equipment design and manufacturing for throughput, efficiency and quality.
Novel idea of common weld tooling as applied in the 2019 Acura RDX inner and outer front door ring system allows for reduction in investment cost. Major enablers to innovation include very tight tolerances in the production of the laser welded blanks that drove higher content of pre-developed holes and near net shape in the hot stamped parts. This reduces the amount of laser trimming required after hot stamping, enabling overall cost optimization of solution.
Continued evolution of inline Non-Destructive Testing (NDT) ensures for a robust solution. Laser welded blanks enabled door ring designs help save more weight than ever before, making cars safer for multitude of crash scenarios and enabling new product attributes like standard panoramic moon-roof system on the 2019 Acura RDX.
Hot Stamped Laser Welded Blanks (LWB) continue to promote safer, stronger, lighter and greener cost effective solutions in steel for the automotive OEMs globally.
To meet regional fuel efficiency and emission standards, vehicle mass reduction has become a major driver for OEMs. Additionally the worldwide shift towards electrification combined with other safety and technology demands will drive automotive manufacturers to aggressively pursue lighter weight vehicles. Increased use of structural adhesives is expected to provide the strength required and the corrosion barrier between traditional and nontraditional materials. In designs where the stiffness of materials or components may be a concern, utilization of structural adhesives can improve noise, vibration and harshness (NVH) and crash performance through a more complete joining surface. New BETAMATE™ Light Weight Reinforcement (LWR) technologies are customizable, highly toughened and range from zero to varying levels of expansion. These new systems are true structural reinforcement solutions available in a range of modulus. BETAMATE™ LWR replaces structural tapes addressing labor and application inconsistencies and enables better gap bridging reliability. They can be used to augment the joining of substrates as well as in areas of the vehicle where weld access may be limited and where design gaps vary. The technology has been successfully implemented in applications to reinforce roof skins and panoramic roofs, and body structural reinforcement to improve crashworthiness. Details on the available adhesive bonding solutions, analysis and characterization will be discussed.
If you have feedback about the GDIS™ past presentation tool, please email Sarah Burns at sburns@steel.org.